Hey folks, let’s cut to the chase—if you’re reading this, chances are you’re either a tool and die maker tired of battling poor surface finishes on your EDM parts, or you’re scoping out how to actually program the control system for a mirror finish die sinker EDM machine. I’m a rep with a die sinker EDM supplier (you know the kind that actually backs their gear with real support, not just a sales sheet) and I’ve spent way too many late nights troubleshooting control programming headaches with shops just like yours. Let’s break this down like we’re chatting over a coffee, no stuffy engineering jargon that makes your eyes glaze over. Mirror Finish Die Sinker EDM
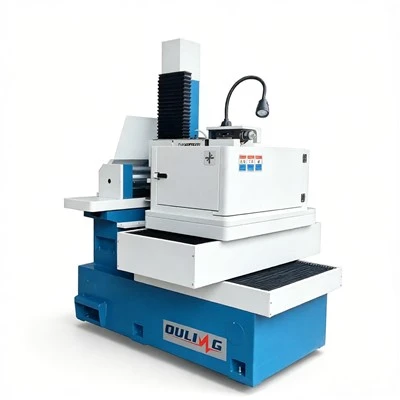
First, let’s get one thing straight: a mirror finish die sinker EDM isn’t your run-of-the-mill hole-popping EDM. The control system here is the brains—mess that up, and even a $100k machine will spit out a finish that’s good enough for a drawer, not a mold for a $100k automotive part or a medical implant that needs to glide through the body. I’ve seen new operators crank up the amperage because they think “bigger spark = faster material removal,” only to end up with a surface that looks like a moon crater, not mirror polishable. So step one: forget the old-school EDM logic that worked for roughing. Mirror finish is a slow, precise dance, not a race.
Let’s start with accessing the right control modes. Most modern mirror finish EDM controls have a dedicated “mirror finish” module, but a lot of new operators just skip that and wing it with general EDM settings. I always tell folks: that module isn’t just a marketing gimmick. It’s pre-programmed with spark cycle timings, gap controls, and servo feeds calibrated for surface roughness values (Ra) down to 0.05 microns—like, glass-smooth stuff. But you can’t just plug in your part program and hit “go.” You’ve gotta tailor it to the electrode you’re using, because copper and graphite act totally different on these machines. Graphite burns faster, so you need a shorter pulse on time, while copper needs a slightly longer on time to maintain a stable gap without arcing. I’ve had a customer use a graphite electrode and crank the mirror mode’s default on time (which is ~10 microseconds) to 15, and they ended up with black spots on the mold—turns out graphite can’t handle that long an on time without building up carbon debris.
Next up: gap control programming. This is where most people mess up. The control’s gap sensor is constantly measuring the distance between the electrode and the workpiece, right? For roughing, you want a wide gap to let debris flush out, but for mirror finish, you need a super tight, consistent gap—like, within 0.1 microns. Wait, no, make that even tighter. If the gap’s too big, the spark goes wild and you get uneven material removal, which kills the finish. If it’s too small, debris can’t escape, leading to short circuits and craters. The control’s servo feed rate is tied directly to gap measurements, but you have to tweak the “gap offset” in the program. I usually set that to 12% of the spark gap for mirror finish—don’t go higher than 15%, that’s a hard no. I once had a shop set it to 20% because they thought it would speed up production, and they wasted two days rework a mold for a consumer electronics case that was supposed to have a mirror finish for the logo. Moral of the story: production speed takes a backseat here. Mirror finish is about quality, not rushing.
Then there’s pulse parameter programming—this is the core of the control system. Let’s get the basics straight: pulse on time (Ton) is how long the spark is active, pulse off time (Toff) is the pause between sparks, and peak current is how strong the spark is. For mirror finish, Ton’s gonna be way shorter than roughing—we’re talking 1 to 5 microseconds, max. I’ve seen guys use 10 microseconds and wonder why their finish is rough. Wait, but don’t go below 1 microsecond, either—some controls can’t maintain a stable spark there, leading to random micro-arcs that show up as tiny blemishes. Toff is equally important. If Ton’s 2 microseconds, Toff needs to be at least 8 microseconds to let all debris flush out before the next spark. I know, that adds up, but again—speed is not the goal here. Peak current? Keep it under 2 amps, even for medium-sized electrodes. I’ve had a shop use 5 amps on a small electrode and ended up with a finish that was Ra 0.2 microns instead of Ra 0.08. It’s a difference no one notices at first, but when the mold cycles 100k times, that rough spot wears out and ruins the part.
Wait, let’s talk about flushing—this isn’t just a setup thing, you program it into the control, too. Most mirror finish EDMs have internal flushing nozzles, but if you don’t set the flushing pressure and timing right, debris gets trapped in the gap. The control has a flushing sync function—you can program it to pulse the flushing at the same rate as the spark cycle. For mirror finish, I set the flushing to turn on for 10% of the Toff time. Too much pressure, and it pushes the electrode around, causing dimensional errors. Too little, and debris stays. I’ve had a customer skip the flushing sync and just use constant low pressure, and they ended up with a “orange peel” finish that looked like bad furniture. Fixing that required a full re-program of the control’s flushing parameters, cost them a day of production.
Now, electrode wear compensation—this is another part of the control that a lot of operators ignore. When you’re doing mirror finish, even a tiny amount of electrode wear (like 0.01 microns) will throw off the finish because the spark gap’s consistent. The control’s electrode compensation feature lets you input wear data in real time, but you have to set it to update every 10 strokes or so. Wait, no—let me correct that: for mirror finish, update it every 5 strokes. Roughing can do 20, but mirror finish needs tighter compensation. I once had a shop that only compensated every 50 strokes, and by the time they finished, the electrode was worn unevenly, leading to a slight step on the mold that the customer noticed immediately. That’s the kind of mistake that makes you lose a repeat client.
Also, don’t sleep on the control’s “spark gap mapping” function. A lot of newer mirror finish EDM controls have this, where it scans the surface before cutting to map the gap across the entire part. You can program it to adjust parameters in real time if the gap changes in different areas—like, if the part has a deep pocket vs. a flat area, the control will tweak Ton and flushing to keep the finish consistent. I always tell operators to run a quick mapping cycle before the actual burn, even if it adds 10 minutes. It saves hours of rework.
Wait, let’s cover a common mistake I see: mixing roughing and mirror finish in the same program. Some guys will rough 90% of the part, then switch to mirror finish in the same program, but they forget to reset the control parameters. The roughing settings (like 10 microsecond Ton, 5 amp current) will creep into the mirror finish section, leading to rough spots. Always make a separate program for mirror finish, or use a subroutine in the control that resets all parameters when you switch modes. That’s a simple tweak, but it’s saved so many shops from headaches.
Now, let’s talk about maintenance tied to the control—because programming doesn’t stop when you hit “run.” The control needs regular calibration of the gap sensor, right? If the sensor’s off by even 0.2 microns, the entire spark cycle is wrong. I recommend calibrating it before every mirror finish run, not once a month. Also, keep the control’s software up to date—manufacturers release updates that fix control logic for mirror finish, like adjusting spark timings for new electrode materials. I had a shop that skipped an update and was getting inconsistent finishes, and once they updated, it fixed itself. No new programming needed, just a simple software push.
Wait, let’s get real for a second: not every job needs the absolute Ra 0.05 micron finish. Sometimes a mold for a plastic toy only needs Ra 0.1, and you can tweak the programming to be a little faster, with 6 microsecond Ton and 1.5 amp current. The control’s flexibility is key here—don’t use a one-size-fits-all program. I always tell customers to test a small, inconsequential area first, like a corner, with their settings, before running the entire part. That way, if something’s off, you don’t waste hours on a big expensive mold.
Let me wrap this up with a quick checklist, because I know you’re scrolling for actionable stuff: 1. Never use roughing settings for mirror finish—use the dedicated mirror module, tweak Ton to 1-5 microseconds, Toff to 8-20 microseconds, peak current <2A. 2. Set gap offset to 12% of the spark gap, use flushing sync at 10% of Toff. 3. Update electrode compensation every 5 strokes. 4. Run gap mapping before cutting, and test a small spot first. 5. Keep control software updated and gap sensor calibrated before every run.
Look, I get it—programming a mirror finish die sinker EDM control is way different than the old EDMs you might be used to. It’s not about cranking numbers to get speed, it’s about precision and consistency. If you’re still winging it with general EDM settings, you’re leaving money on the table and dealing with rework that eats into profits. I’ve seen shops that switched to proper control programming for mirror finish cut their rework rate by 80% in the first month.
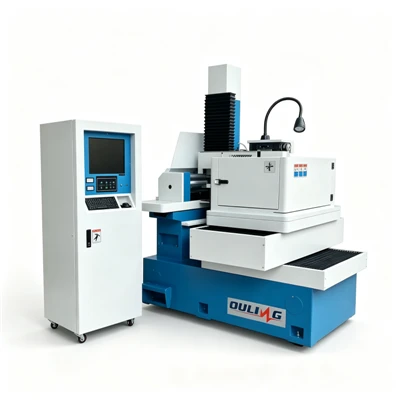
If you’re looking for a mirror finish die sinker EDM machine (or just need help tweaking your existing control programming to get that perfect mirror finish) hit us up for a chat. No hard sell, just real advice from people who’ve been doing this for years. We’ll walk through your specific setup, adjust your control settings, and make sure you’re getting parts that look and perform exactly like you need. Don’t waste another batch of parts guessing—let’s make your next mirror finish burn count.
Mirror Finish Die Sinker EDM References: 1. Rajur, K. P., & McGeough, J. A. (1998). Advances in Electrical Discharge Machining. CIRP Annals – Manufacturing Technology, 47(2), 591-608. 2. Tönshoff, H. K., et al. (2000). Mirror Finish EDM: Fundamentals and Applications. Journal of Materials Processing Technology, 107(1-3), 15-21. 3. American Society of Mechanical Engineers (ASME). (2015). Standard Guide for Electrical Discharge Machining (EDM). ASME B94.55M-2015.
Taizhou Ouling CNC Equipment Co., Ltd.
As one of the most professional mirror finish die sinker EDM manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced mirror finish die sinker EDM made in China here from our factory. Welcome to contact us for quotation.
Address: No. 9 jingang Road, Yangzhou City Jiangsu Province, China
E-mail: 574751243@qq.com
WebSite: https://www.oulingedm.com/
